Food & beverage
Hygienic conveying and packing-line integration for dairy, ice cream, confectionery, tea and dry goods.
- Nestlé
- Danone
- Juhayna
- Froneri
- Mondelēz
- Kraft Foods
- Kellogg's
- Mars
- Bel
- Almarai / Beyti
Conveyors and material-handling equipment for food, personal-care and industrial plants, from the first drawing through fabrication, controls and installation on site.
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
 Open in 3D →
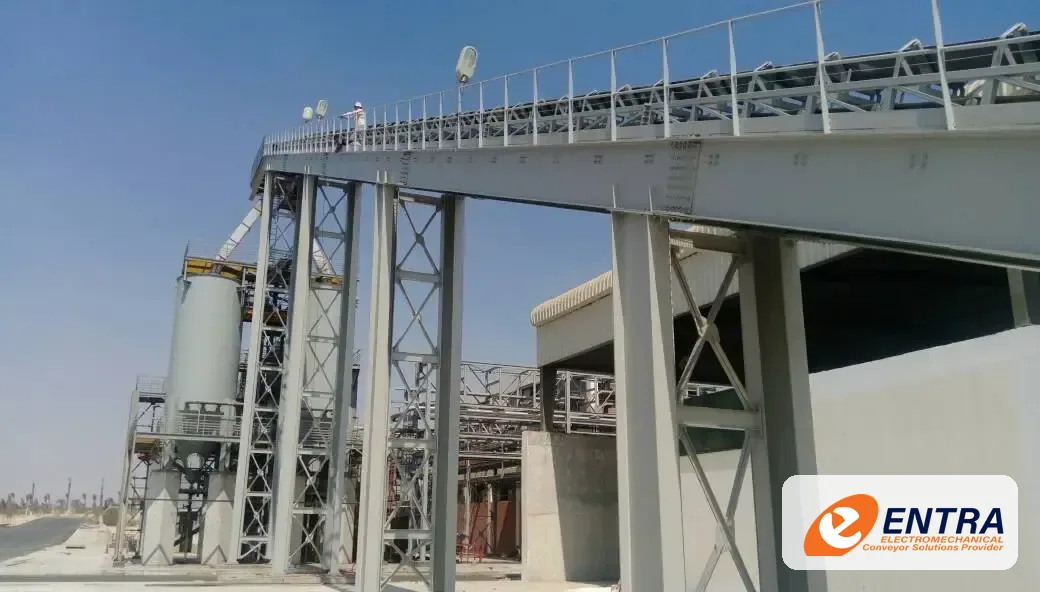
Footage from ENTRA projects: manufacturing, installing and running conveyor and material-handling systems in factories.
Drag to rotate, pinch or Ctrl + scroll to zoom, and tap the orange points to identify the main components. Use Explode to separate the assemblies and Fullscreen for a closer look.
Loading 3D scene…
Answer four simple questions. We’ll suggest a suitable ENTRA solution, explain how it works and show you what to consider next. No engineering knowledge needed.
Your result is a helpful starting recommendation. Our team will confirm the final design after reviewing your product, layout, capacity and operating conditions.
Conveyor, material-handling and line-integration work by ENTRA, sorted by type of equipment.
ENTRA works with food, personal-care, heavy-industry and manufacturing plants. Hygiene, safety and space requirements differ in each, so the solution does too.
Hygienic conveying and packing-line integration for dairy, ice cream, confectionery, tea and dry goods.
Packing-line conveyors, stainless steel transfers and modular chain systems for household and personal-care plants.
Heavy-duty belt conveyors and steel structures for bulk material and process plants.
Material flow, pallet handling and line integration for manufacturing and packaging operations.
Based on ENTRA's client reference list, including P&G, Nestlé and Danone sites.
What each client needed, what we built, and photos from site.
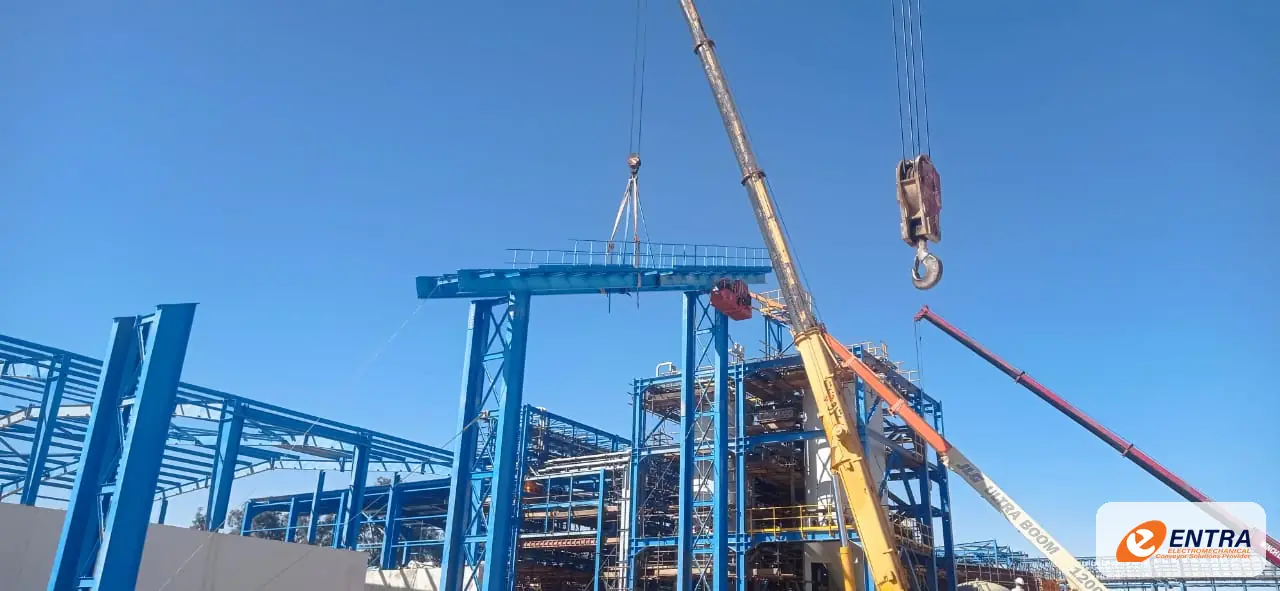
Client: Al Nasr Chemicals
Industry: Chemicals, energy & heavy industry
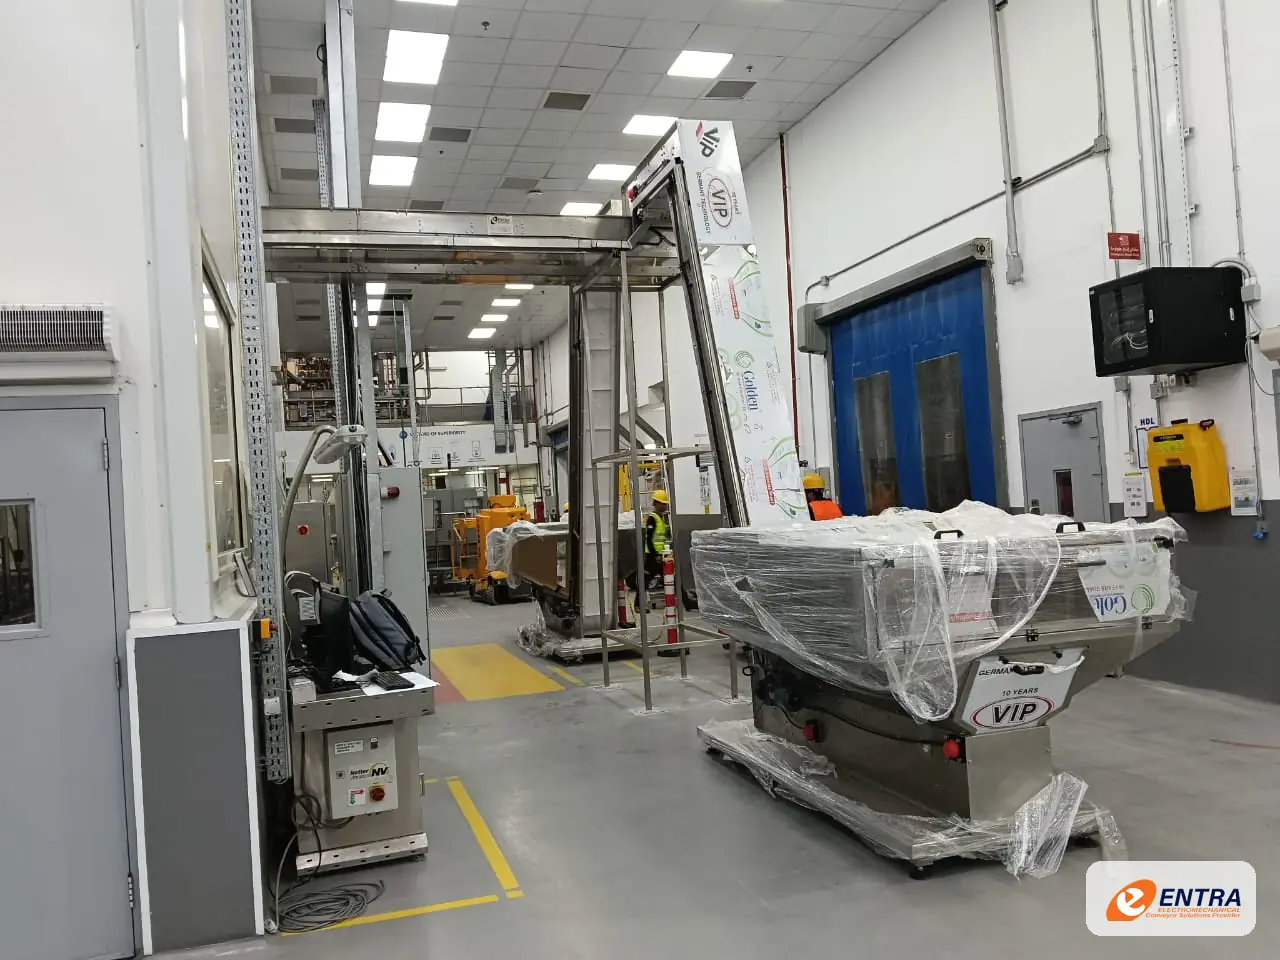
Client: P&G Egypt
Industry: Home & personal care
Filter by type or search by name. Each card opens a short preview, the product page or the 3D model.
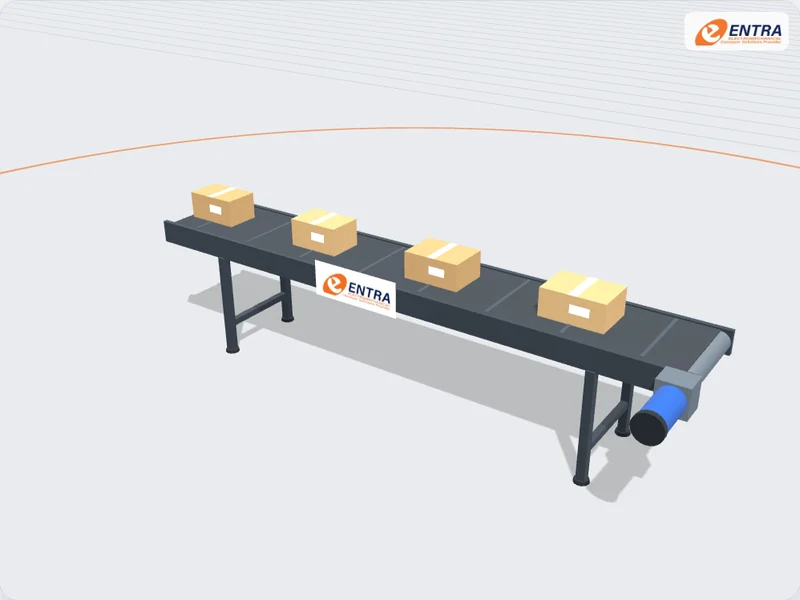
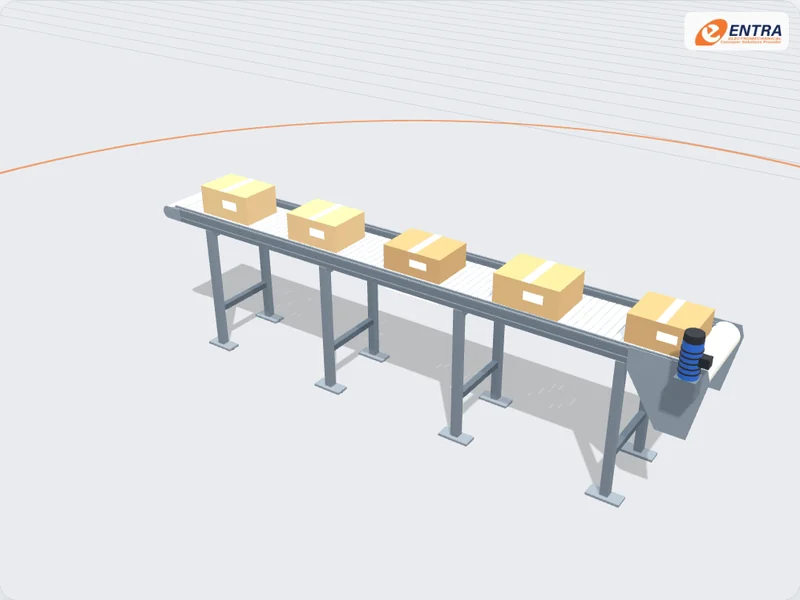
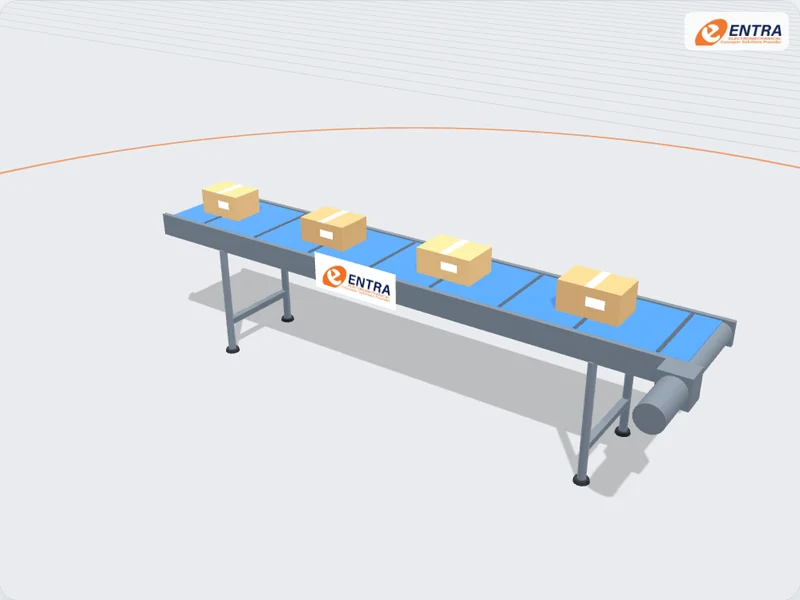
A continuous belt runs over a drive drum and a tail drum to carry cartons, cases, bags and unit loads. Built flat or as a cleated incline between levels.
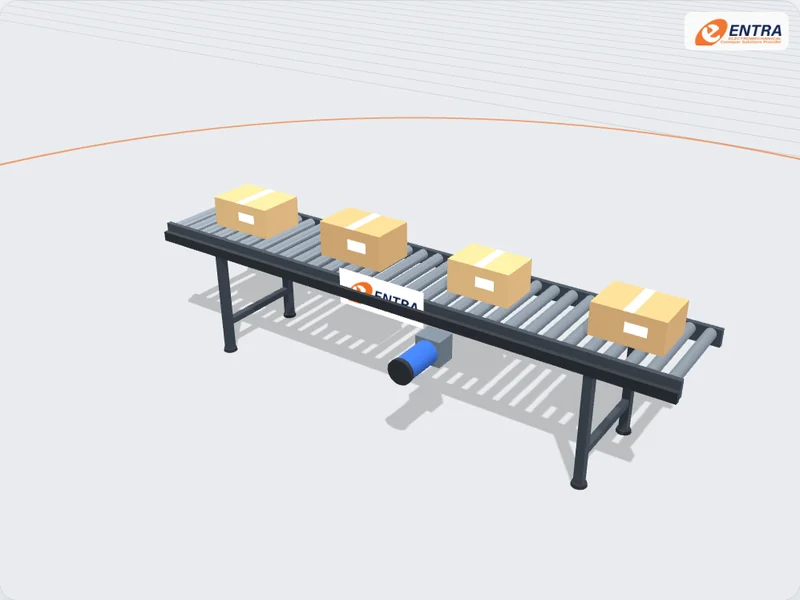
Loads travel on a bed of rollers. Gravity sections use a slight slope or a manual push; powered sections drive the rollers for transport and accumulation.
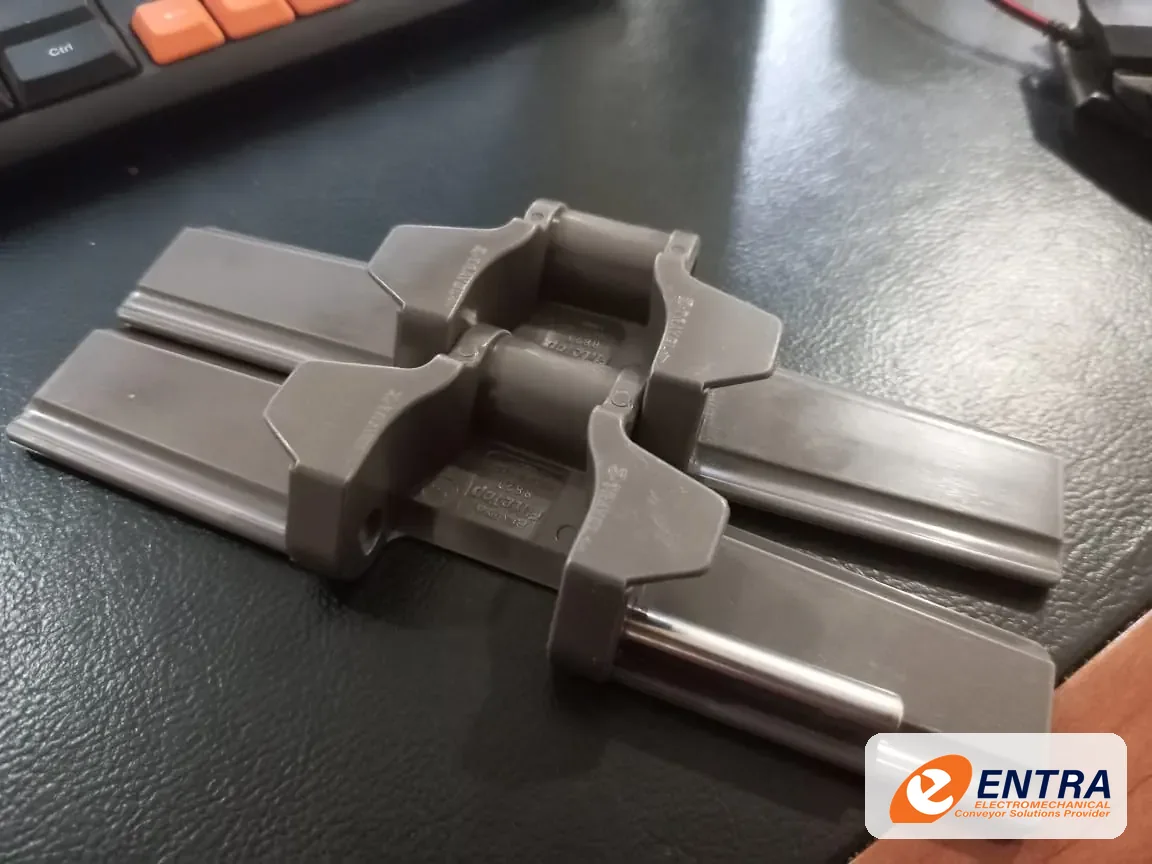
An aluminium beam guides a plastic chain on low-friction slide rails. Five chain widths carry items from 15 mm to 500 mm wide.
A free-turning wheel carries the chain round a tight radius. It has the lowest friction of any bend.
One chain and one drive follow the route your floor allows. Wheel bends come in 30°, 45°, 60°, 90° and 180°.
A friction-top chain climbs up to 25° without the product slipping back. Plain chain is limited to about 7°.
A plastic modular belt for wider and heavier products, in 315, 435 and 585 mm widths.
Products ride on pallets carrying RFID tags, so each one can be stopped, located and tracked through the line.
A conveyor built on slotted aluminium profiles, so guides, sensors and stands bolt on anywhere and the line is easy to extend or reconfigure.
A conveyor with a stainless-steel structure and an open, cleanable frame for process areas where corrosion resistance and washdown matter.
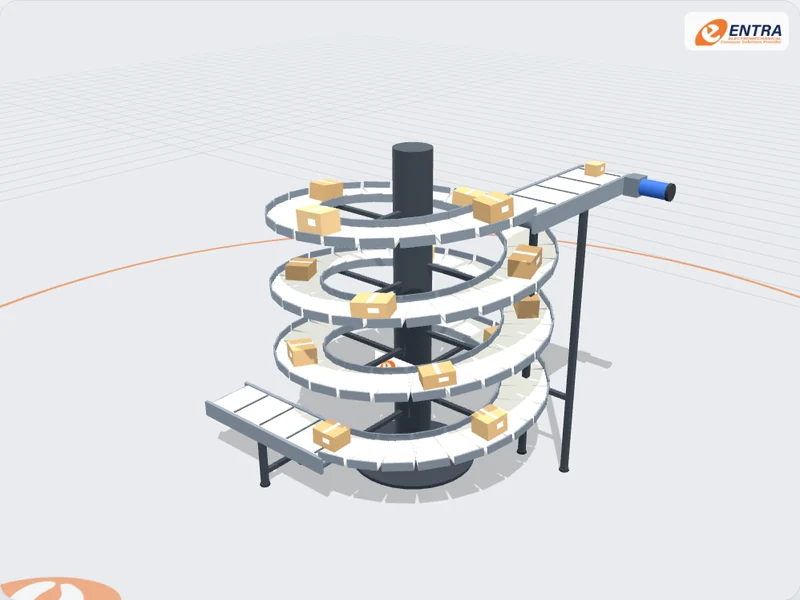
Products climb or descend on a continuous helical track around a central column, changing level in a small footprint without stopping the flow.
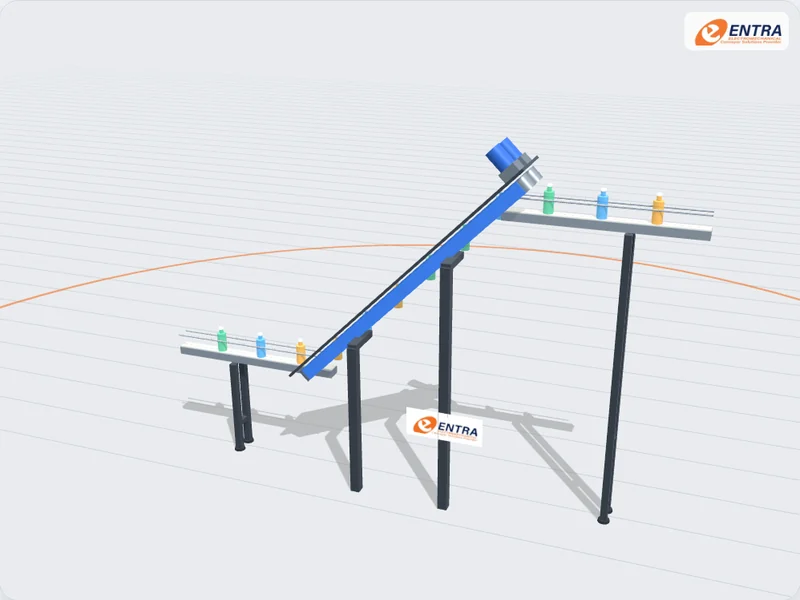
Two opposing belts hold each container by its sides and carry it steeply up or down between conveyor levels, keeping it upright.
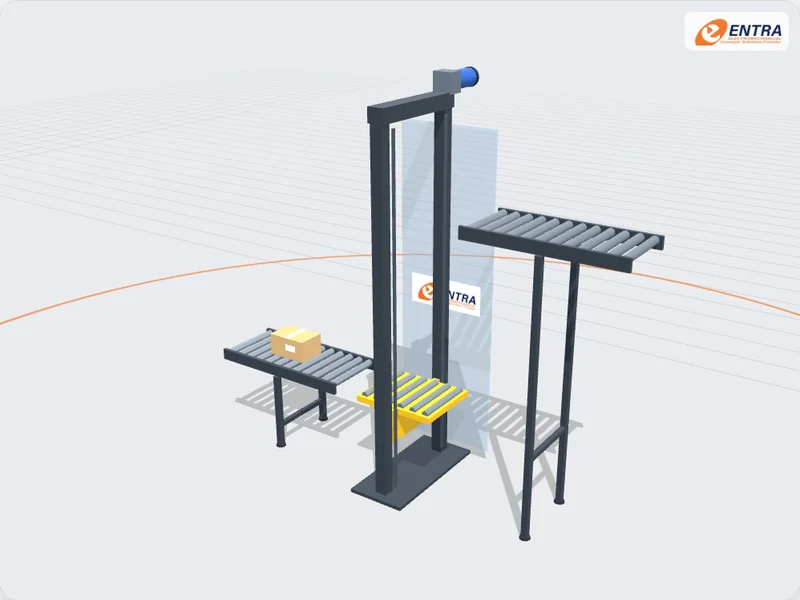
A guided carriage lifts or lowers the load between two conveyor levels when a horizontal conveyor cannot bridge the height.
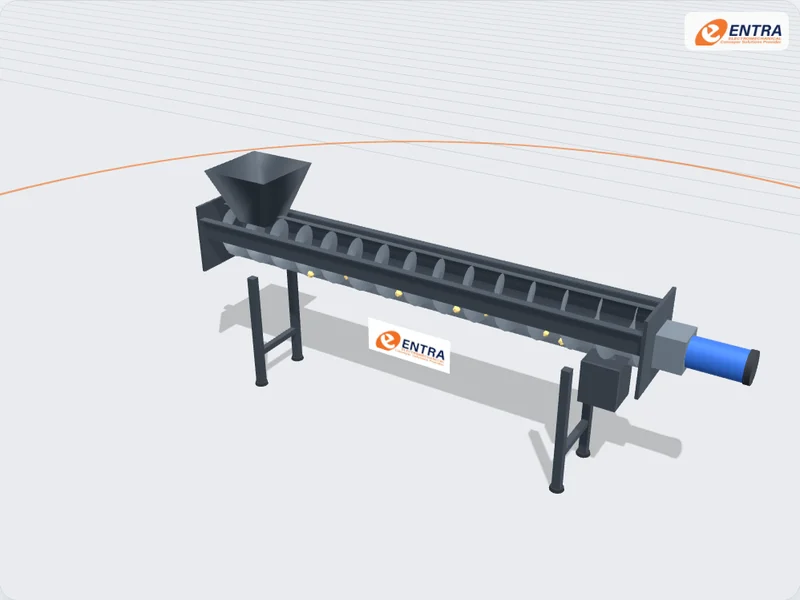
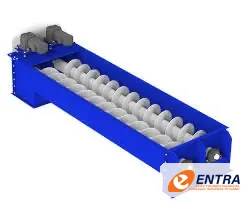
A rotating helical flight pushes powders, grains and other bulk material along a closed casing from the inlet to the discharge.
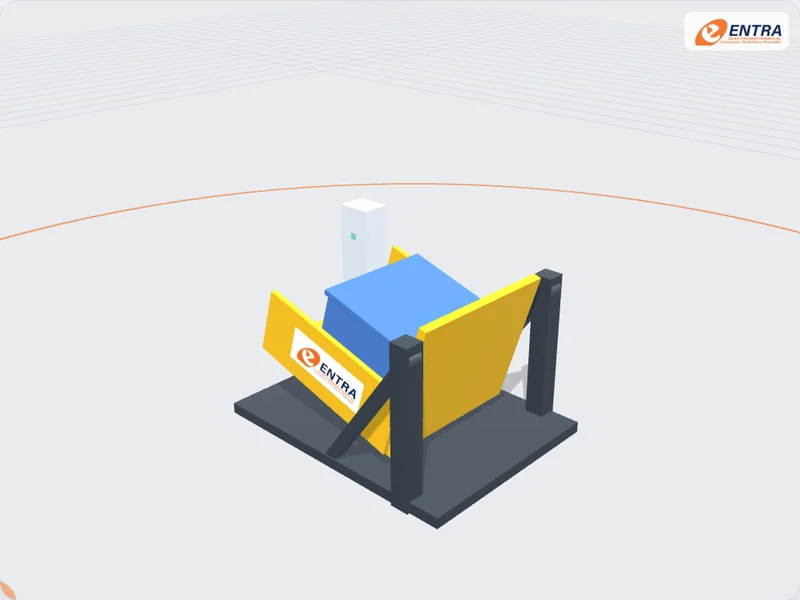
A pivoting cradle holds the load and tilts it to a set angle for emptying, feeding or a change of orientation, then returns it.
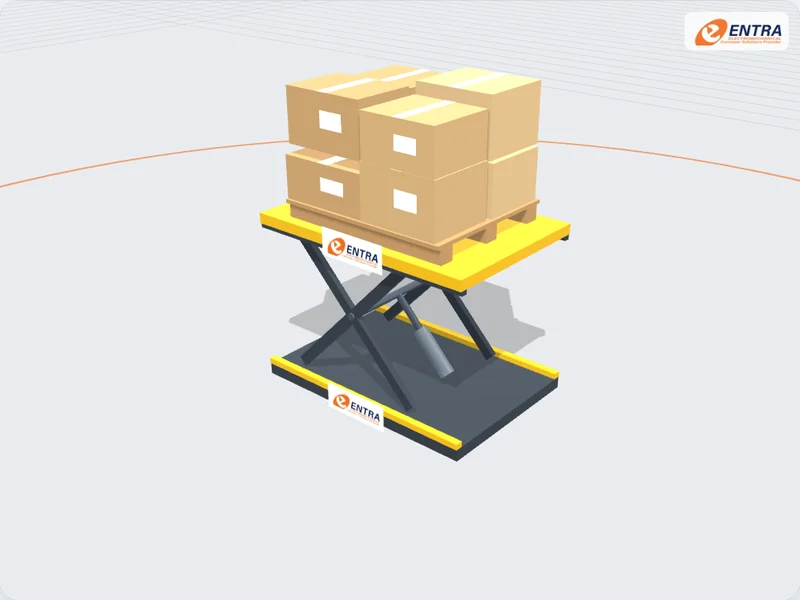
Crossed scissor arms raise and lower a level platform, bringing pallets and heavy loads to a safe working height or to the level of a conveyor.
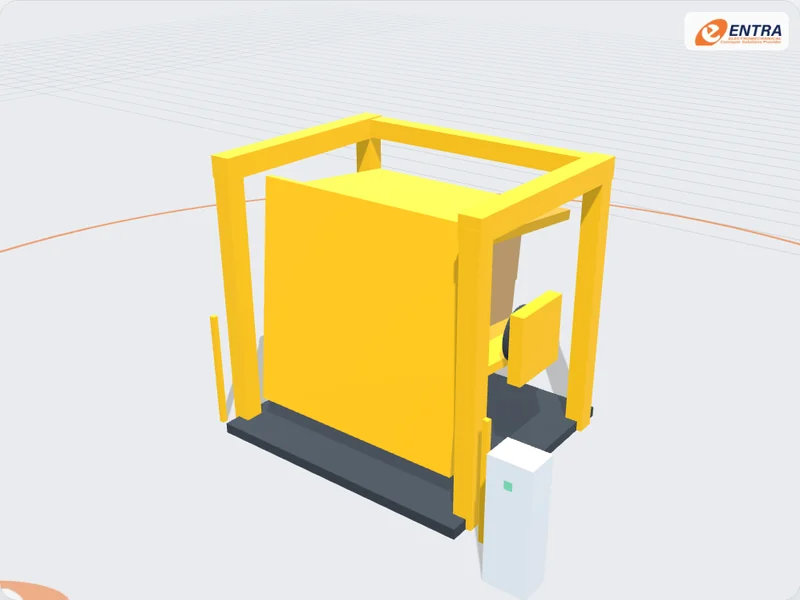
A rotating clamp unit grips a full pallet load between two platens and turns it over, so the pallet can be exchanged or damaged goods recovered without hand restacking.
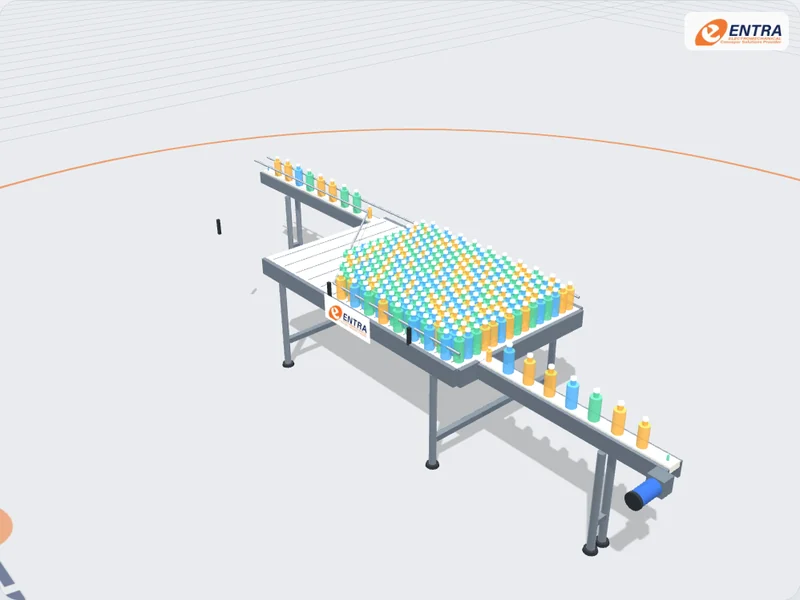
A wide moving bed holds products for a short time when the next machine stops, then guide rails funnel them back into single file so the line keeps running.
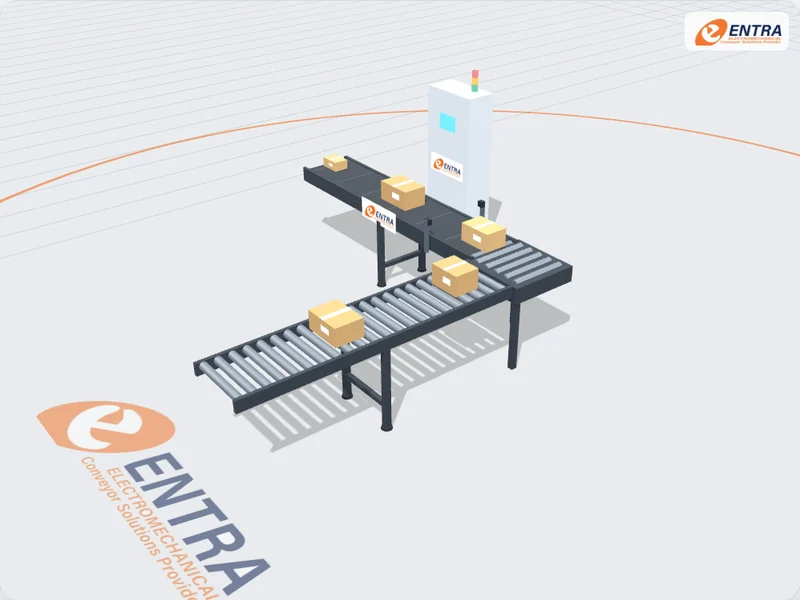
Conveyor sections, a right-angle transfer, sensors and a control panel work as one line, so product flow is coordinated between machines.
No product matches that search.
For each of our 14 product families: how it works, where it is used, the main parts, and what we size it around.
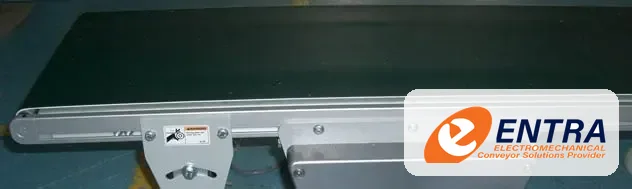
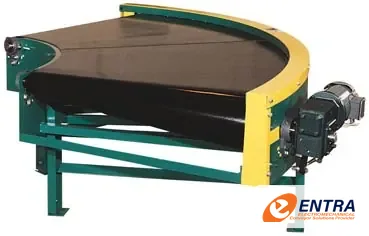
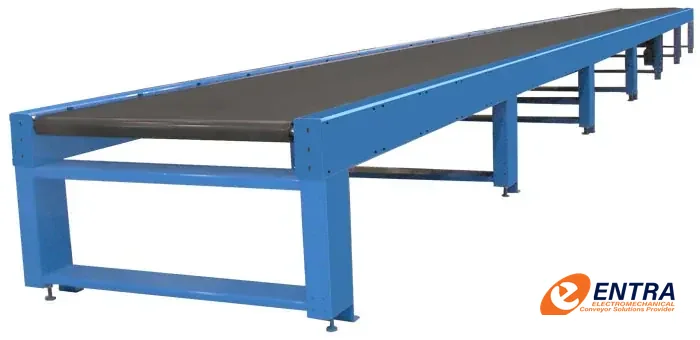
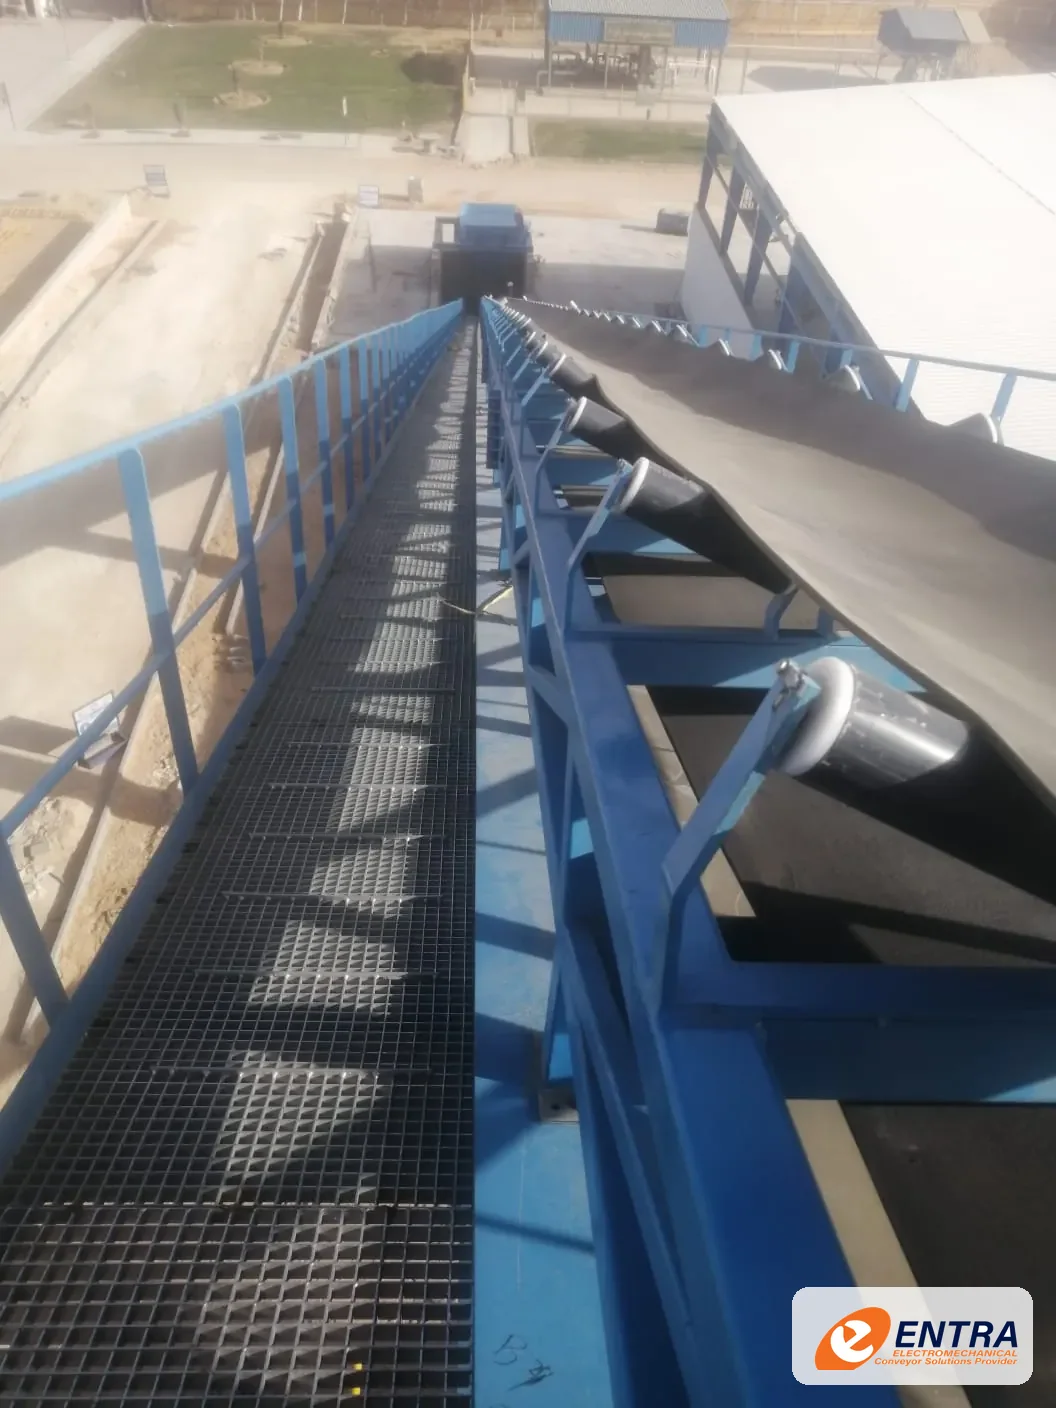
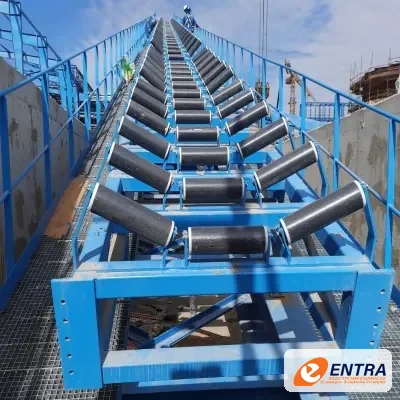
A belt conveyor carries products on a continuous moving belt supported by a frame and driven through a pulley arrangement. Belt material, width, speed, support, tracking and transfer geometry are selected for the product and operating environment. This page describes the equipment family; it is not a fixed standard design.
The gallery photos are ENTRA portfolio references from the belt-conveyor category. No universal belt speed, capacity, width or load rating is published here because these depend on the selected belt, drive, frame and application.
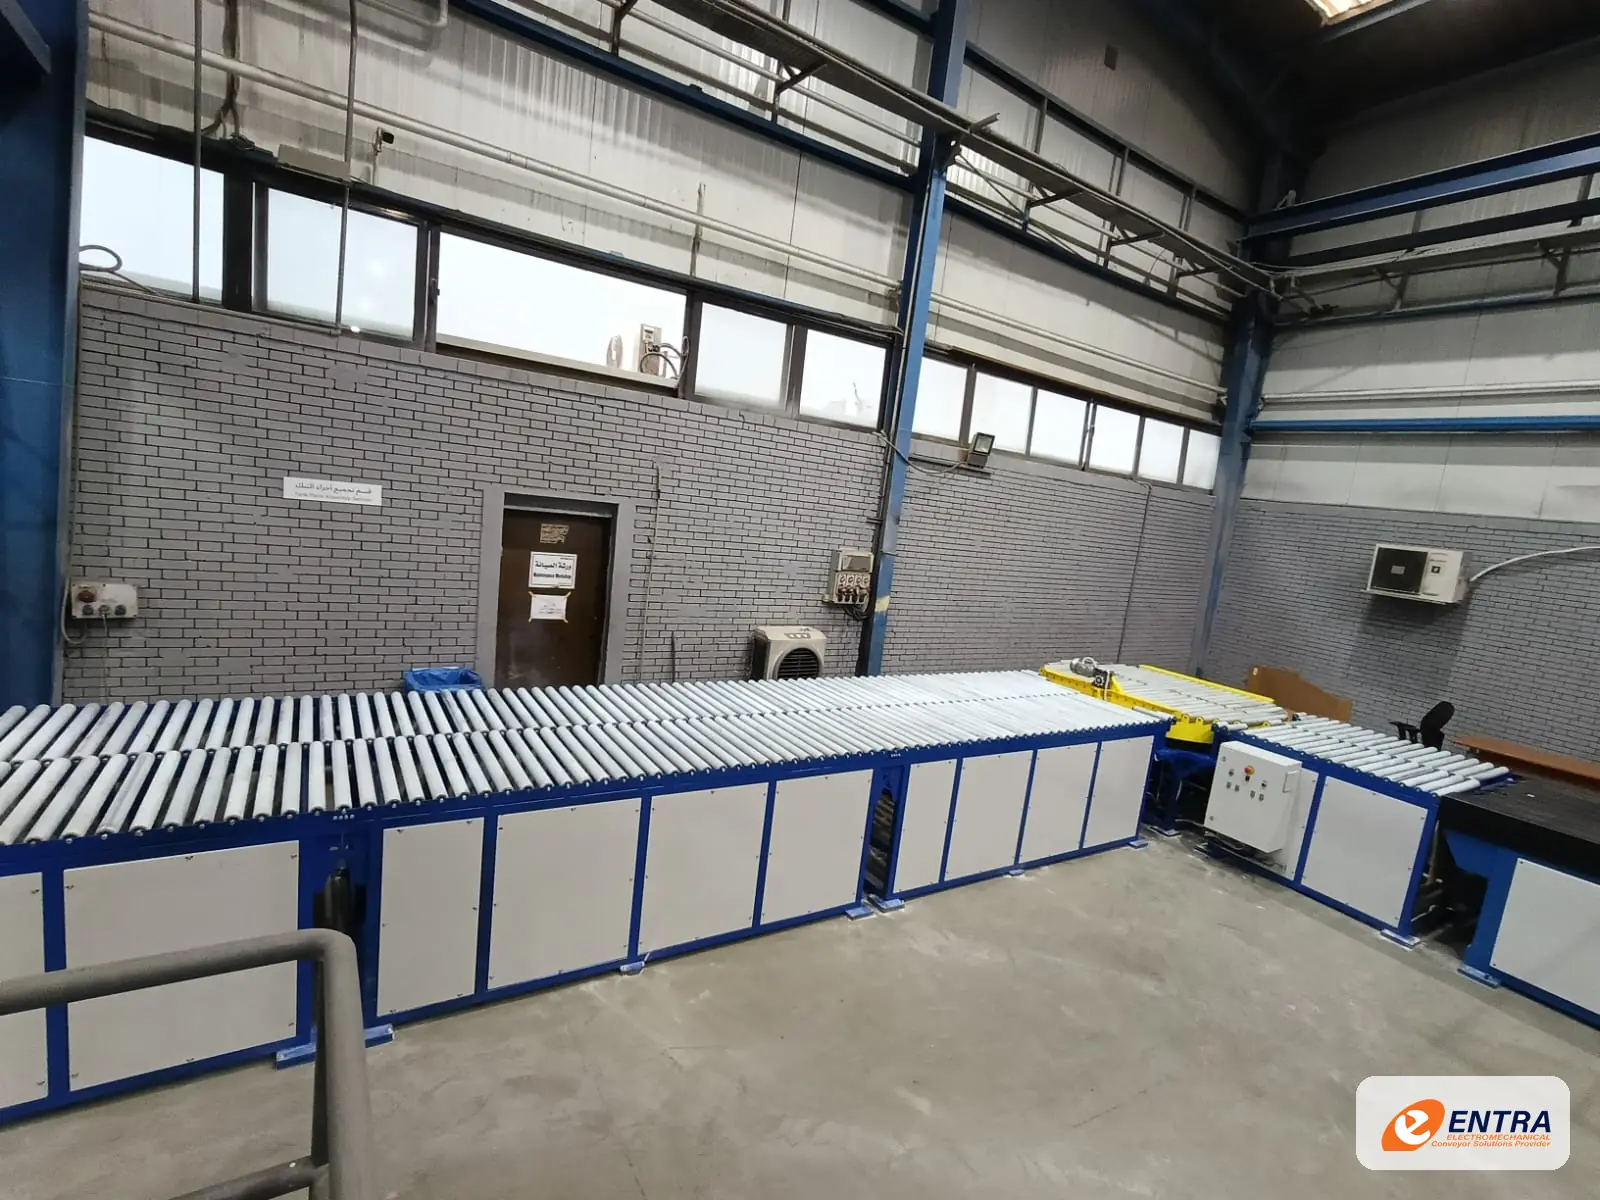
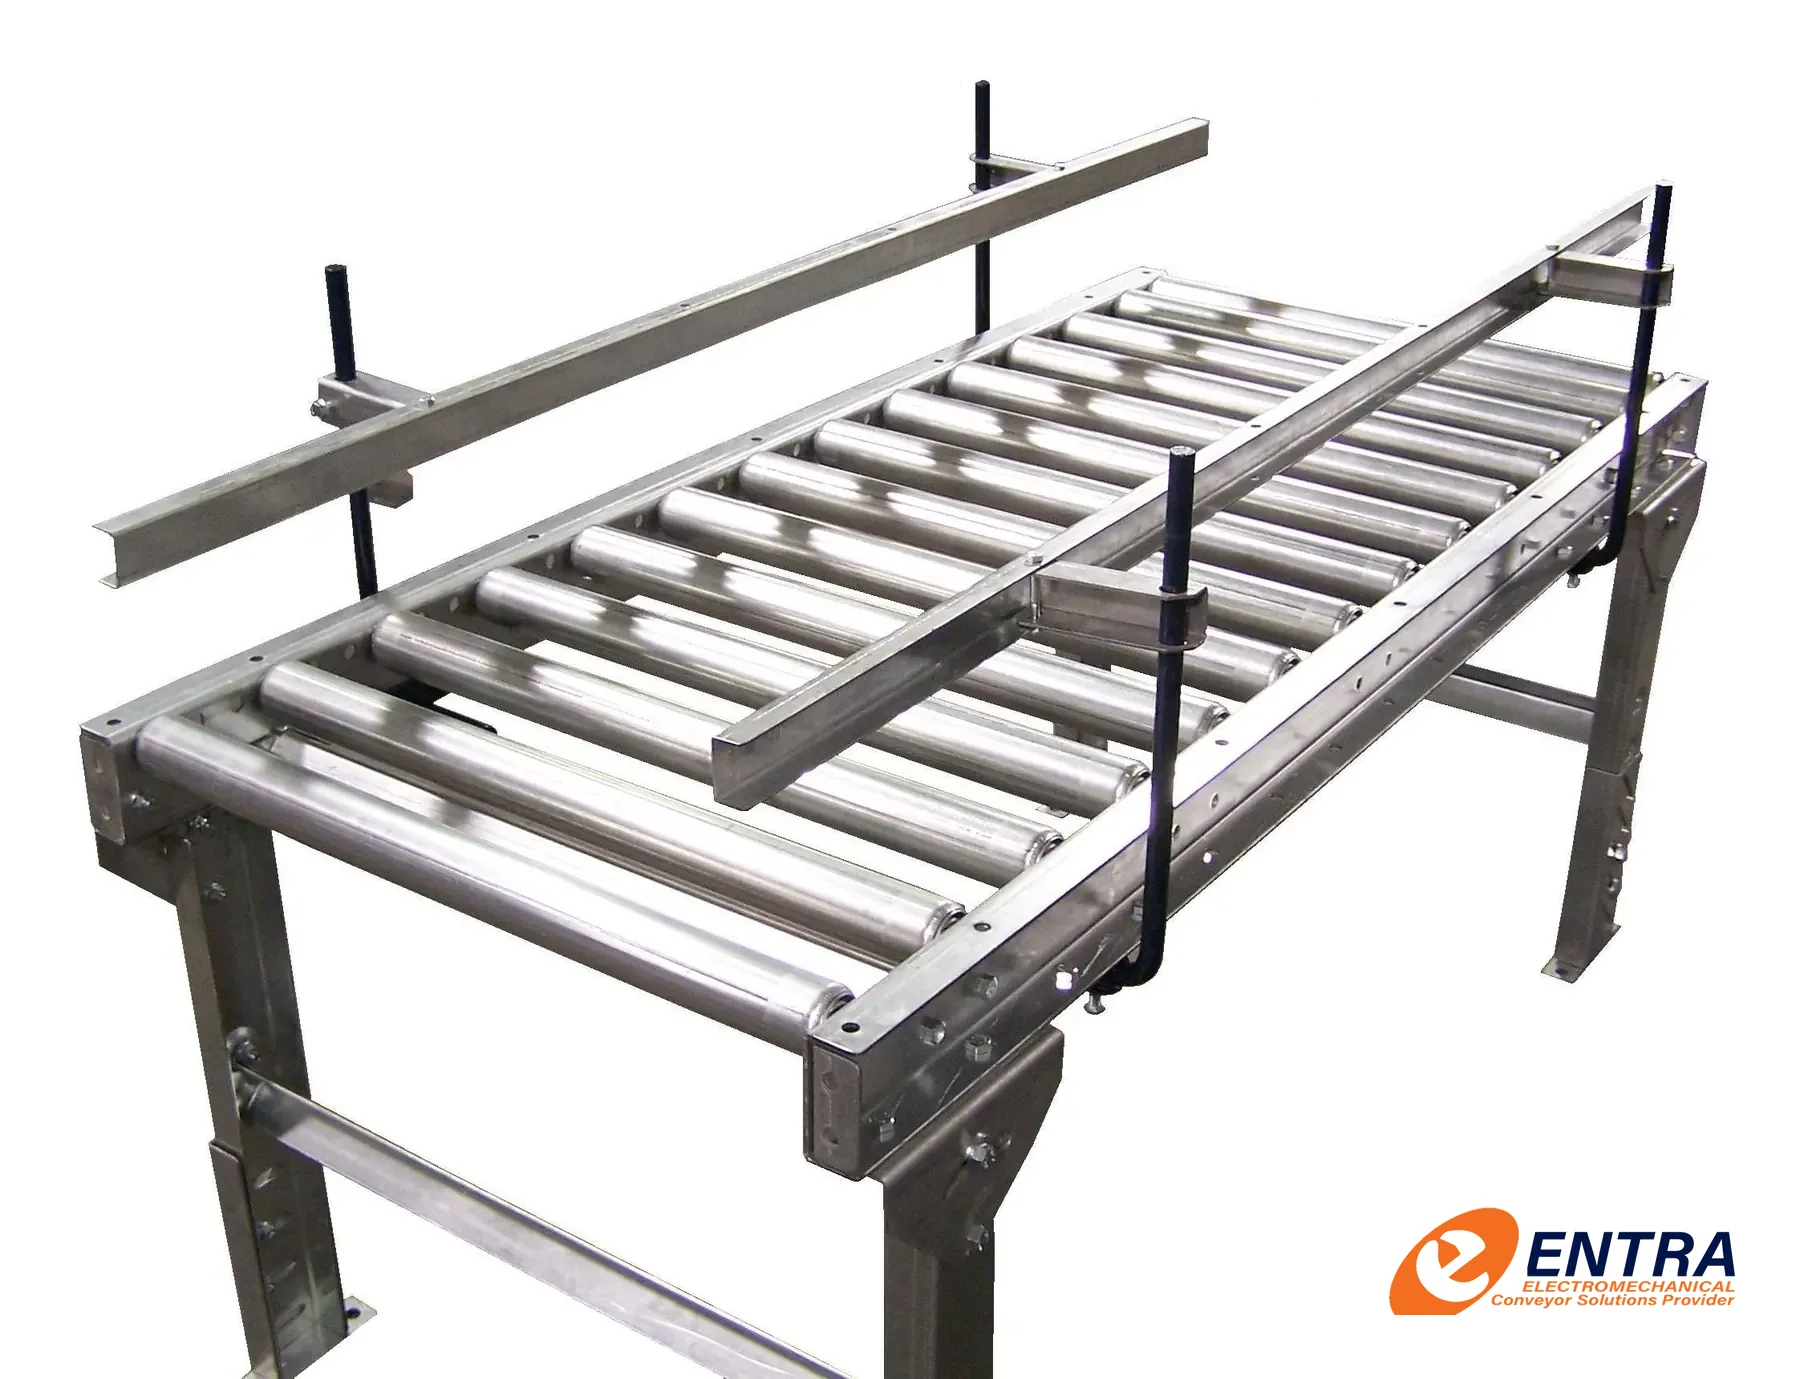
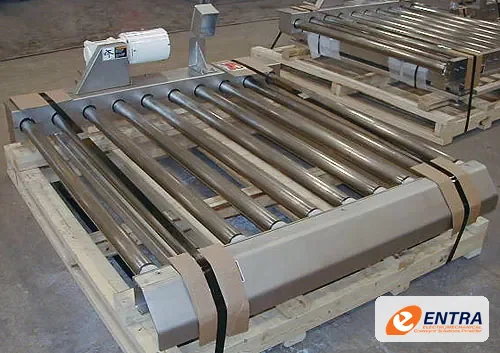
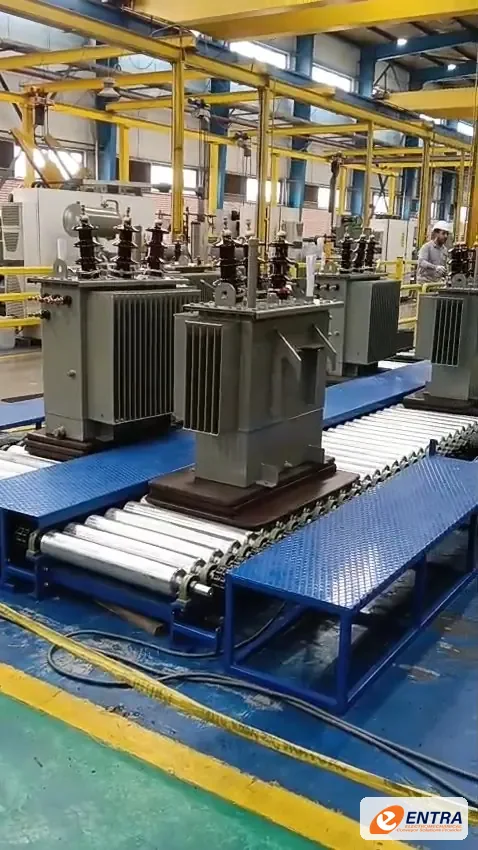
Roller conveyors support products on a series of rotating rollers. Gravity versions rely on slope and product momentum; powered versions drive rollers directly or through belts, chains or line shafts. Roller pitch, diameter, frame and drive zones must suit the load base and product geometry.
Roller conveyor images are from ENTRA’s roller-conveyor gallery. Pallet duty, carton duty and accumulation behavior require different design checks; the same roller layout should not be assumed suitable for every load.
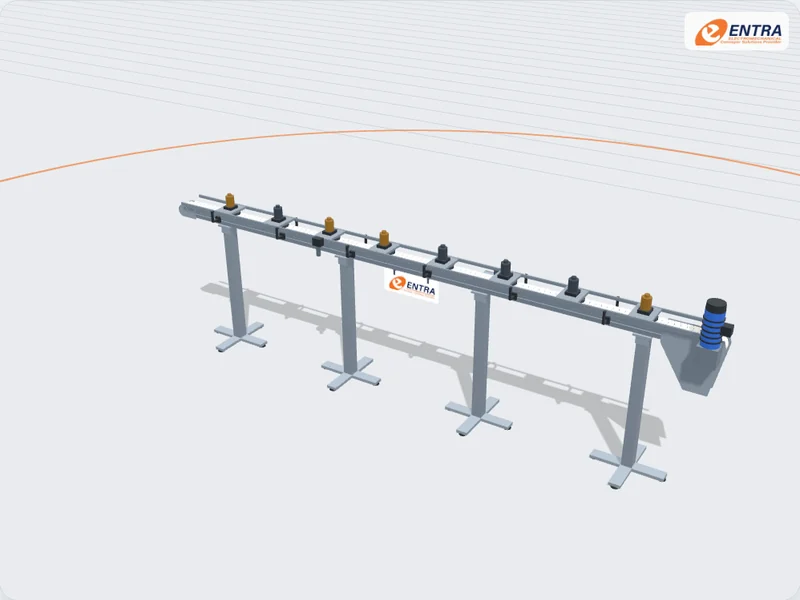
MODU plastic-chain systems use modular links running over compatible wear strips and support profiles. The V22 catalogue identifies aluminium plastic-chain families MP, MS3, MM3, ML2 and MX2, plastic-belt families MT2, MR2 and MF2, pallet families and stainless families. Select the family and polymer only after checking product, duty and environment.
Numerical values above are taken from the MODU Product Catalogue V22 technical reference for POM chain. PP chain data differ. These are catalogue values, not an application approval; confirm exact material, duty, load, temperature, speed, layout and series with ENTRA.
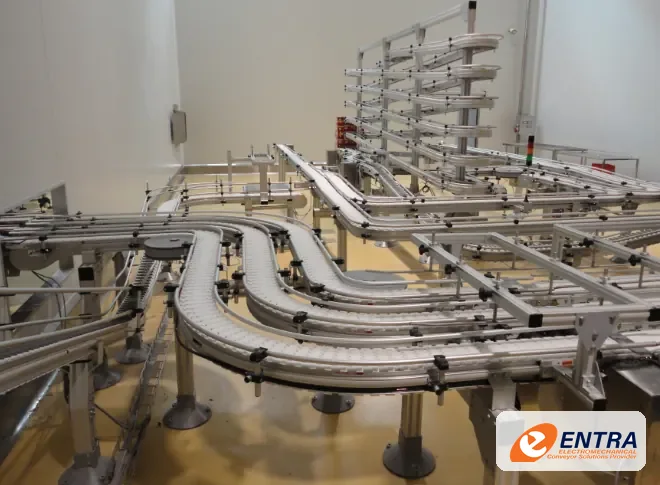
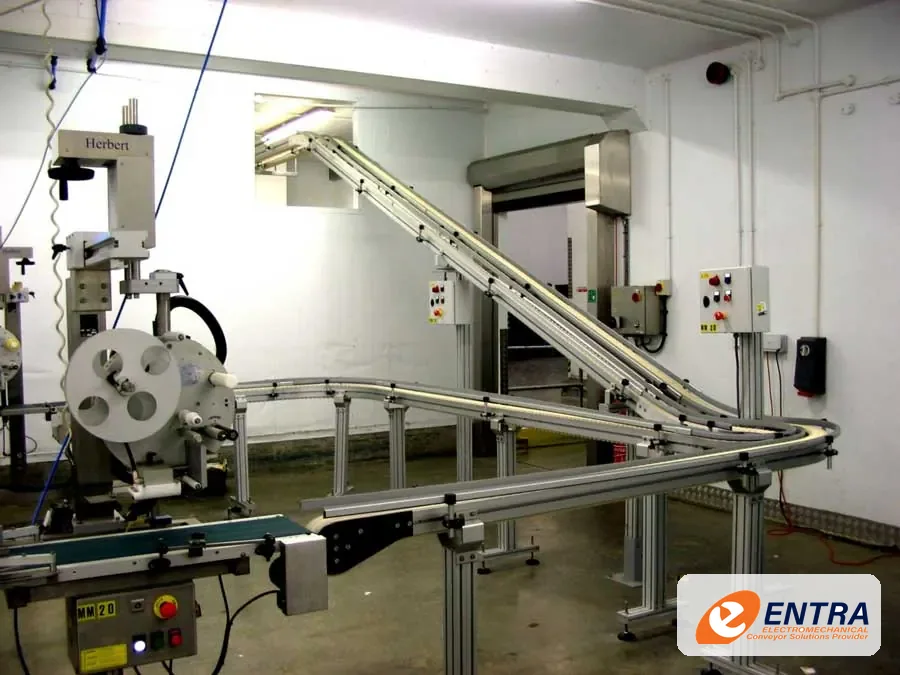
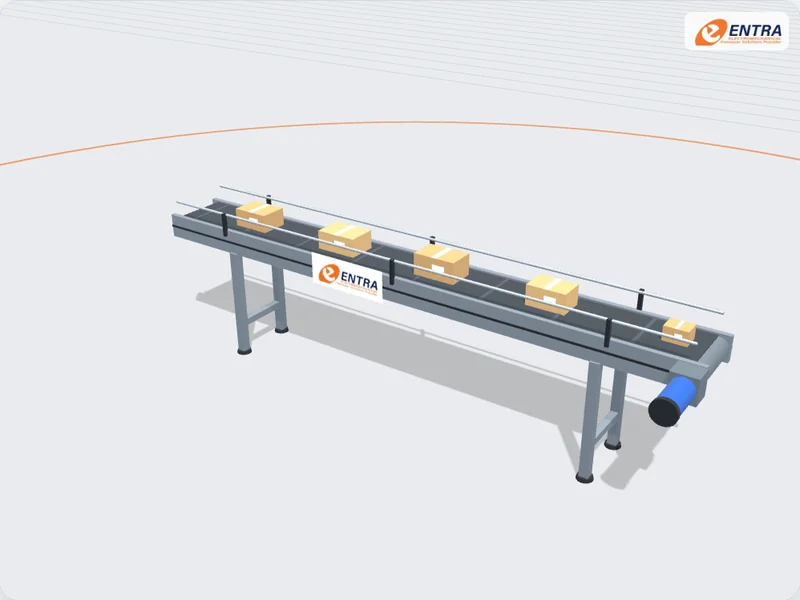
Aluminium-profile conveyors use modular extruded profiles and compatible brackets, supports and guarding to create configurable conveyor frames. The conveying medium may be selected separately—such as belt or modular chain—so frame material alone does not define the conveyor’s load or performance.
The images show aluminium conveyor structures from ENTRA projects. They do not indicate a particular profile series or load rating.
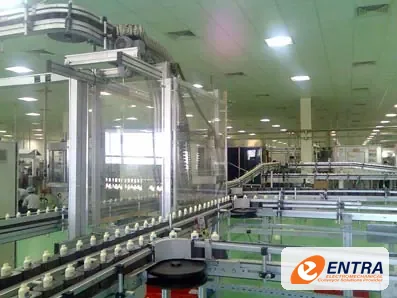
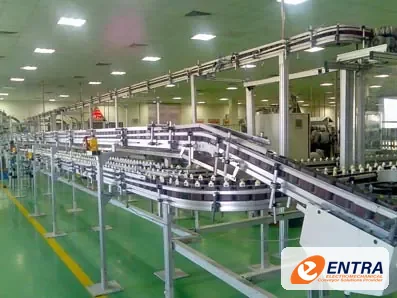
Stainless-steel conveyors are selected where corrosion resistance, cleaning access, product-contact requirements or process conditions call for stainless construction. Stainless steel alone does not make a conveyor hygienic: geometry, weld finish, drainage, seals, bearings, belt materials and cleaning procedures all matter.
No GMP, FDA, IP, ATEX or other compliance claim is implied. Customer standards and required documentation must be identified and reviewed for the specific project.
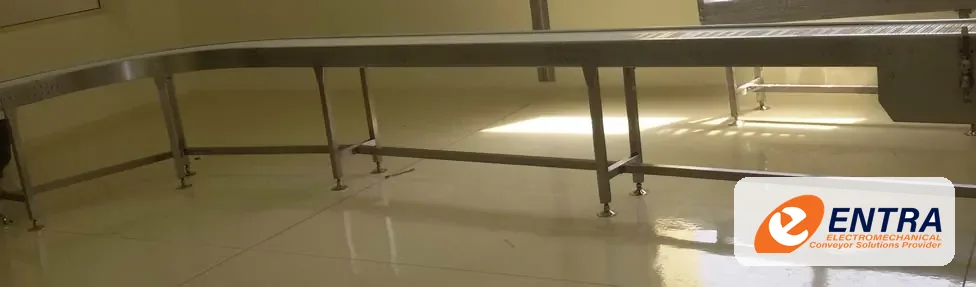
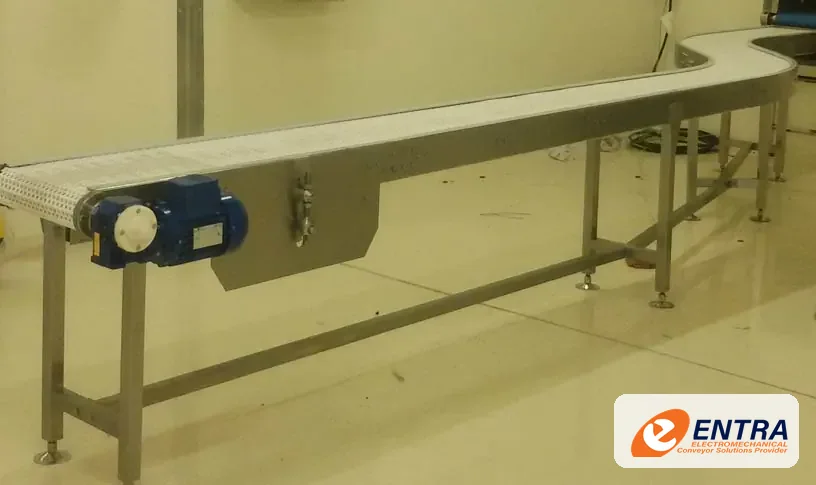
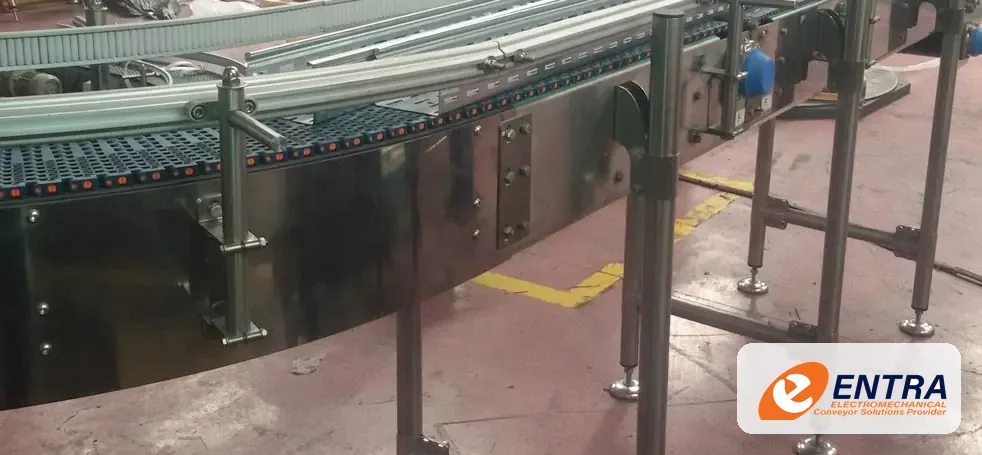
An industrial spiral conveyor transfers products between elevations while maintaining a continuous conveying path. Depending on the belt, product and process, a spiral can be used for elevation, lowering, accumulation, cooling or buffering. The final design is selected around the product and the line—not from a generic height claim.
Spiral capacity, maximum elevation, belt speed, product loading and temperature suitability are project-specific. ENTRA confirms these after reviewing the product, layout, belt selection, drive duty and operating environment. No universal capacity or height is assumed on this page.
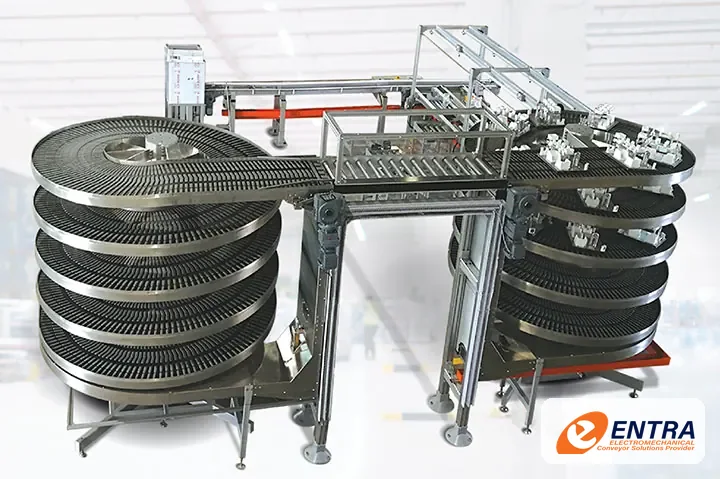
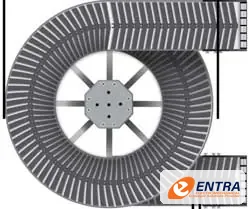
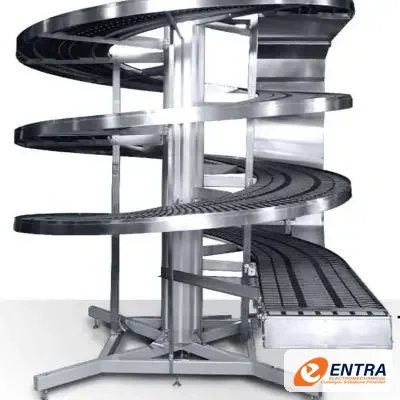
A side-gripper conveyor uses two synchronized, opposing belts or gripping elements to hold a product along its sides while it is transferred. It is useful where a conventional base-supporting conveyor cannot provide the required vertical path or where the product needs to be presented in a controlled orientation. Grip geometry and pressure must be matched to the actual container.
Grip dimensions, pressure, belt speed and achievable throughput depend on the actual container and line layout. Fragile, tapered, wet, slippery or highly variable products require trials or engineering review before a final design is selected.
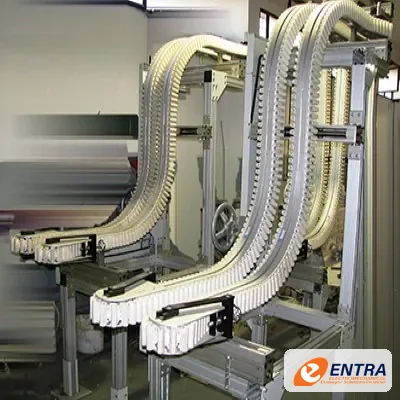
Industrial elevators and lowerators transfer products vertically when a horizontal conveyor cannot bridge the required level change. The lifting principle may use a platform, carrier, cleat, bucket, gripper or other product-specific support. The equipment principle must be selected from the load and transfer duty rather than inferred from the word elevator.
The images show general elevator equipment. No rated load or travel speed is implied.
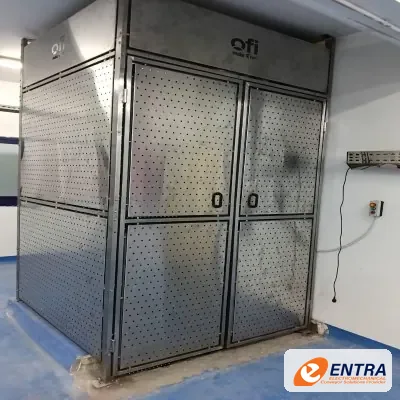
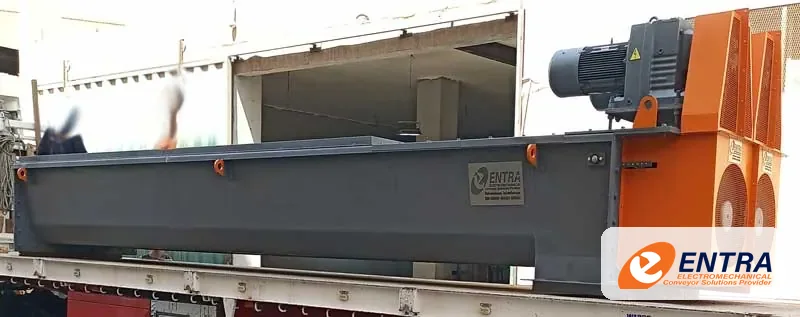
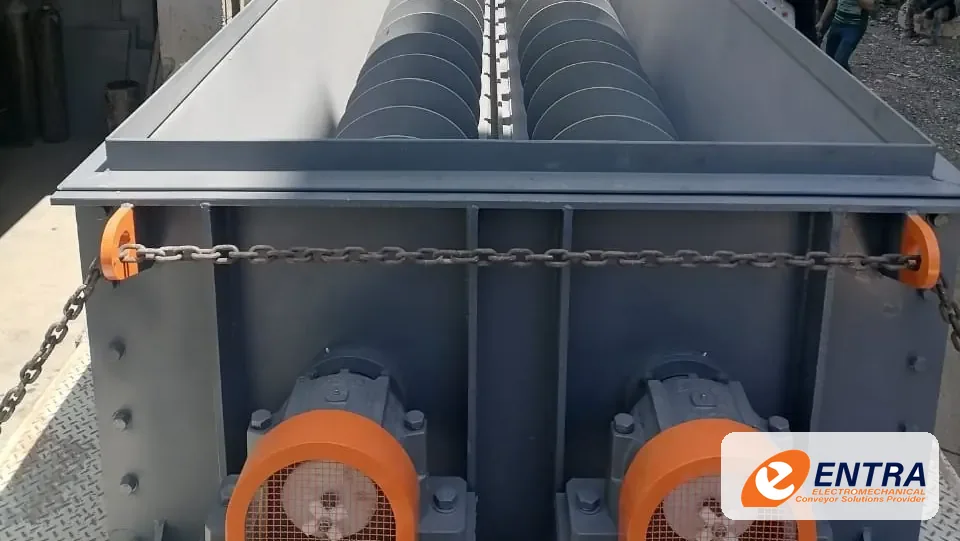
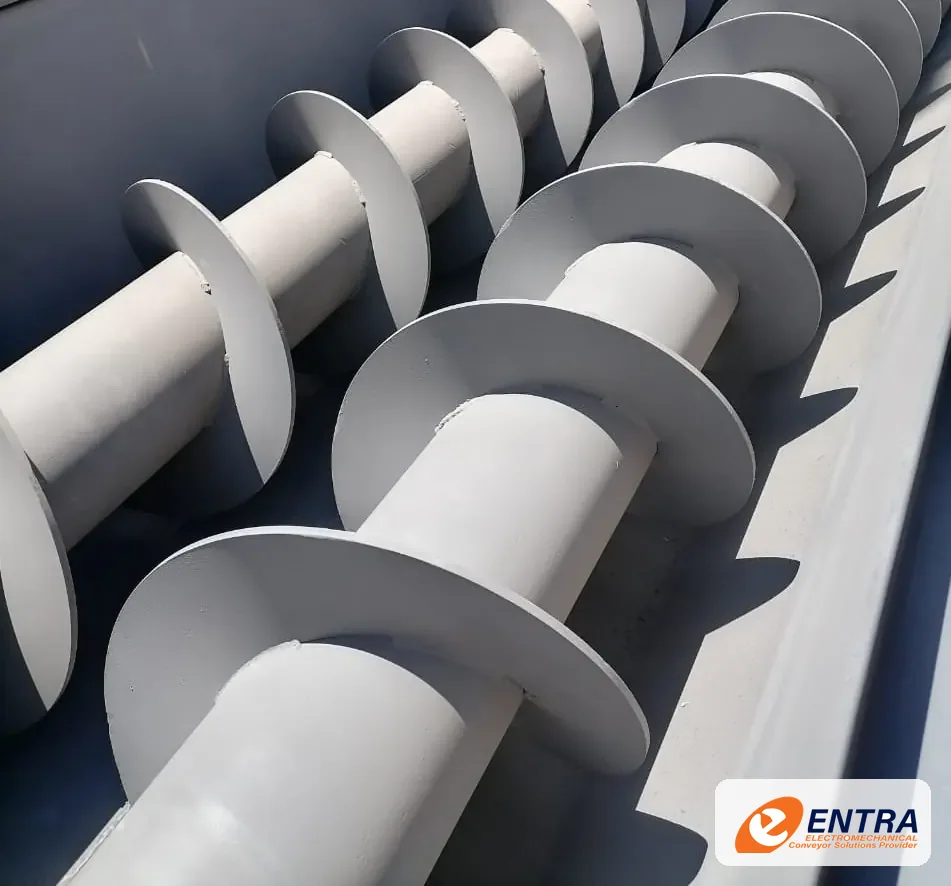
A screw conveyor moves bulk material along a casing by rotating a helical flight around a shaft—or by using a shaftless spiral in suitable applications. It can provide horizontal or inclined conveying, controlled feeding and transfer between process stages. Selection depends heavily on the material properties and the required duty.
Screw conveyor capacity is not inferred from diameter alone. It depends on material bulk density and flow behaviour, flight geometry, pitch, speed, fill ratio, inclination and duty. Abrasive, sticky, hot, combustible or food-contact materials require specific material, sealing, guarding and process review.
Tilting and inverting stations change the orientation of a load to support emptying, access, assembly, inspection or process transfer. The mechanism may use a pivoting cradle, powered table, clamp or purpose-built fixture. Product retention and controlled movement are central to safe design.
The gallery category contains tilting-station equipment references. Do not infer a rated load, tilt angle or safety category from photographs; these are determined by the project design and risk assessment.
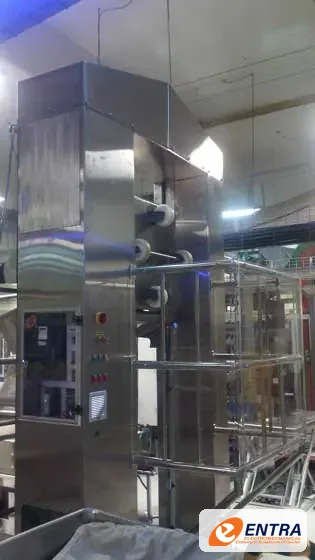
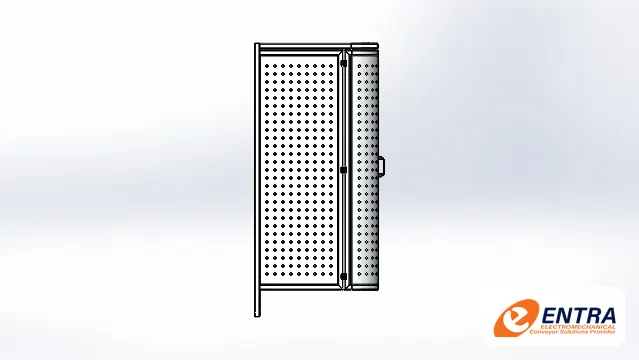
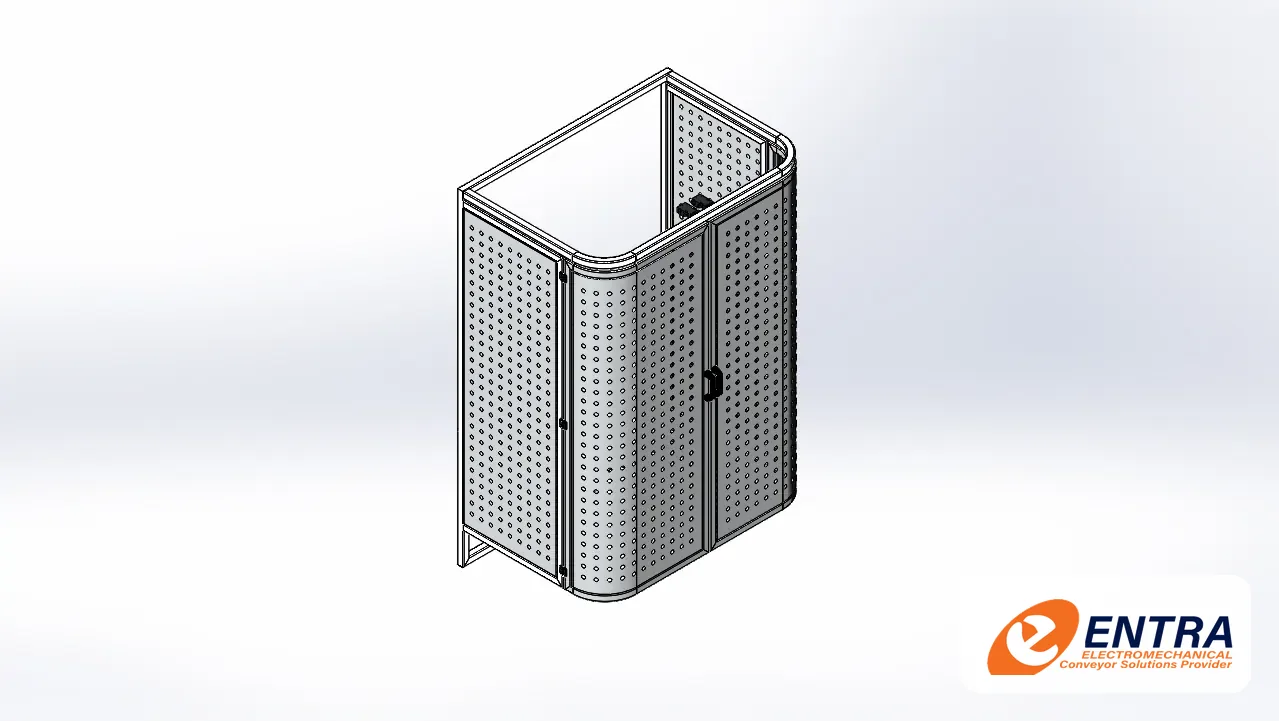
A scissor lift table raises and lowers a level platform on crossed scissor arms driven by a lifting cylinder. It brings pallets, bins and heavy unit loads to a comfortable working height, matches the level of a conveyor or machine, or helps loading at different heights. Platform size, stroke, lifting drive and safety devices are selected for the load and the workplace.
This page shows ENTRA's 3D model of the lift table. Capacities, heights and speeds are defined per project and are not implied here.
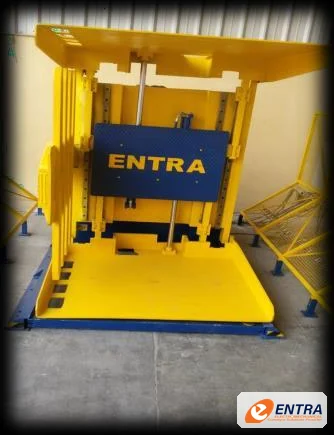
A pallet inverter grips a complete pallet load between two clamping platens and rotates it, typically through 180 degrees. The pallet can then be removed and replaced, for example to change from a wooden to a plastic or hygienic pallet, to recover goods from a damaged pallet, or to turn a load over for a process step. Clamping force, rotation and controls are selected for the load so it stays stable throughout the cycle.
The photo shows an ENTRA pallet inverter from the ENTRA company profile. Capacities and cycle times are defined per project and are not implied here.
An accumulation conveyor momentarily holds products before releasing them to the next production phase. On an accumulation table, products arrive in single file, spread onto a wide moving bed when the downstream machine slows or stops, and are guided back into single file by rails when it restarts. ENTRA supplies accumulation tables and alpine (multi-level) accumulation conveyors.
The photo shows an ENTRA accumulation table. Buffer capacities and speeds are defined per project and are not implied here.
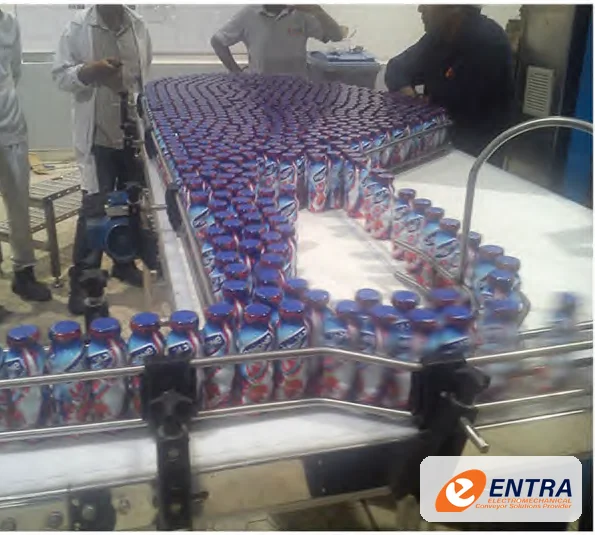
Conveyor line integration connects individual machines and transport sections into a coordinated material-flow system. The engineering scope may include mechanical transfers, accumulation, product detection, drives, PLC interfaces, operator controls, safety circuits and commissioning. Exact automation architecture depends on the existing plant and project scope.
The images are industrial application references from ENTRA projects. They do not assert a specific PLC brand, safety performance level, line throughput or certification.
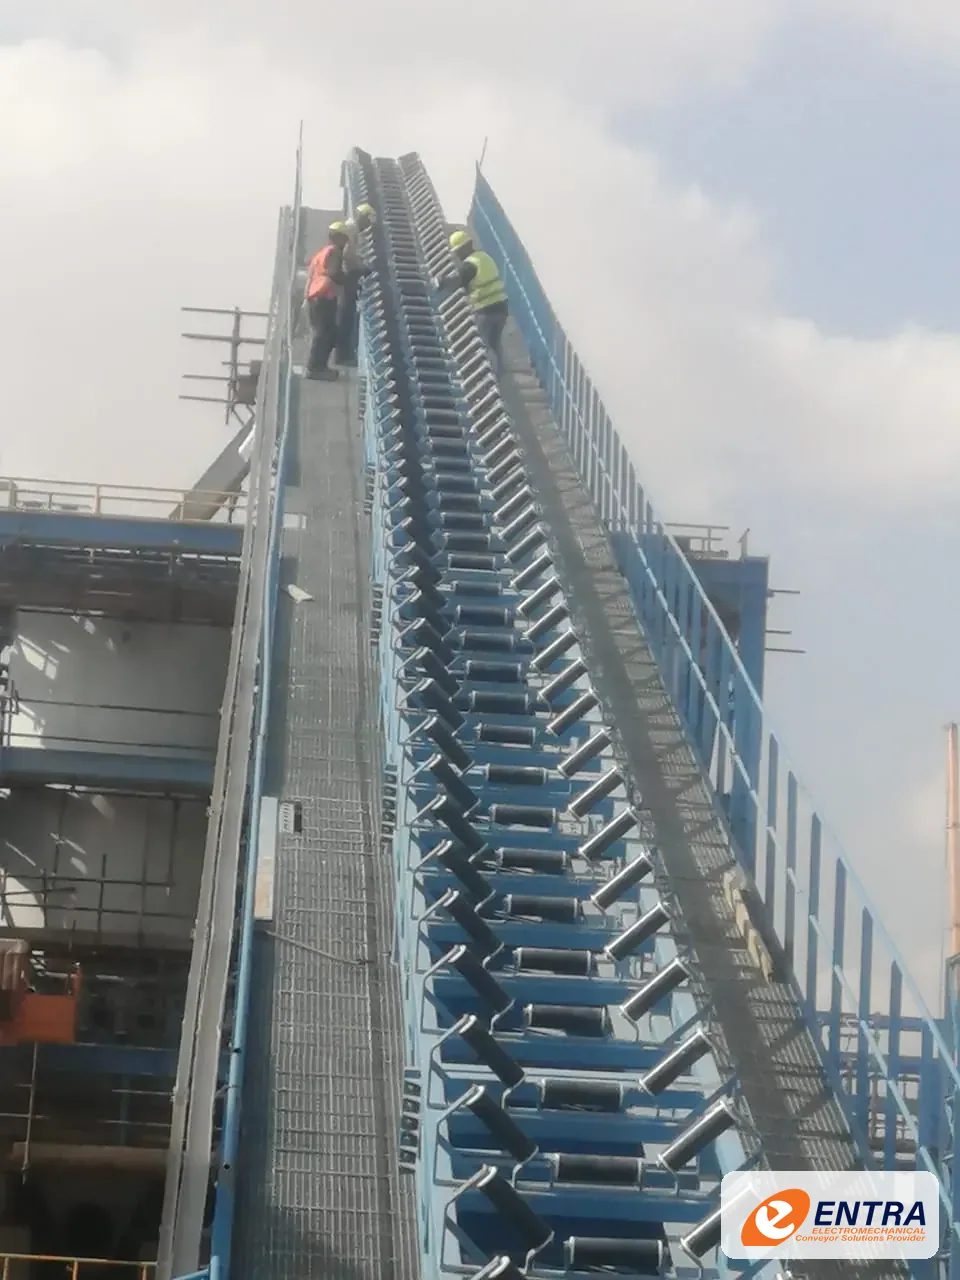
Beyond the systems above, we also build:
Operator platforms, mezzanines and walkways in mild or stainless steel, freestanding or built around a machine, including multi-level process platforms.
ENTRA conveyor support structures, adjustable tripods and bipods, stainless/HDPE guide rails, brackets, drip pans, crossovers and dead-plate transfers matched to your conveyor layout.
Stainless-frame modular chain and belt series (DS2, DM3, DL2, DX2, DT2, DR2, DF2) and the 4-size STC Slat-Top conveyor range for bottling, canning and hygienic packaging lines.
Conveyor lines for composite-can making, carton handling, paper converting, personal-care and pharmaceutical packaging, product assembly and heavy bulk or mining transport.
Photos, 3D models and designs are the property of ENTRA and may not be reused without written permission.
A few lines about your product and factory are enough to start. Attach drawings or photos when you email us and an engineer will follow up.
From food and beverage to personal care, packaging and energy, our conveyor systems run in plants across Egypt, the Middle East and Africa.



Also trusted by Kraft Foods · Fine · Obour Land · Haidylena · Al Nasr Chemicals · Unitel · Olé · Harvest · Aroussa · Brego
Since 2009 ENTRA has represented MODU System, the modular conveyor manufacturer founded in Singapore in 1995, supplying its chain, belt and aluminium conveyor platform with local engineering and support.
Explore the MODU platform →